Nonwoven fabric is a sheet material made by bonding fibers directly — mechanically, thermally or chemically — without weaving or knitting them the way traditional fabric is made. Because it skips spinning and weaving, nonwoven fabric is faster and cheaper to produce, and its thickness and strength can be tuned for anything from load-bearing geotextile to lightweight medical masks.
Most content on this topic stops at selling finished nonwoven fabric. This guide goes further: it explains what machines actually make that fabric — because that’s Vina Nonwoven’s business as the Vietnam distributor of needle-punch and PET spunbond production lines.
Definition: what is nonwoven fabric?
Nonwoven fabric is a sheet or roll material formed from a layer of fiber (a fiber web) bonded directly together, instead of interlacing yarn in two directions the way woven fabric is. The input fiber can be staple fiber (short-cut fiber such as PET, PP, viscose, wool, recycled fiber) or continuous filament (fiber spun and bonded on the same line, as in spunbond).
Fibers are bonded together in one of three ways:
- Mechanical bonding — barbed needles punching through the web (needle punch) or high-pressure water jets (spunlace) that entangle the fibers together.
- Thermal bonding — heat and pressure (calendering) partially melt and fuse the fiber, common in spunbond and meltblown.
- Chemical bonding — a binder or resin holds the fibers together (less common among the machine lines Vina Nonwoven distributes).
Types of nonwoven fabric by production technology
There are four main technologies, each giving fabric with different properties and applications:
1. Needle punch
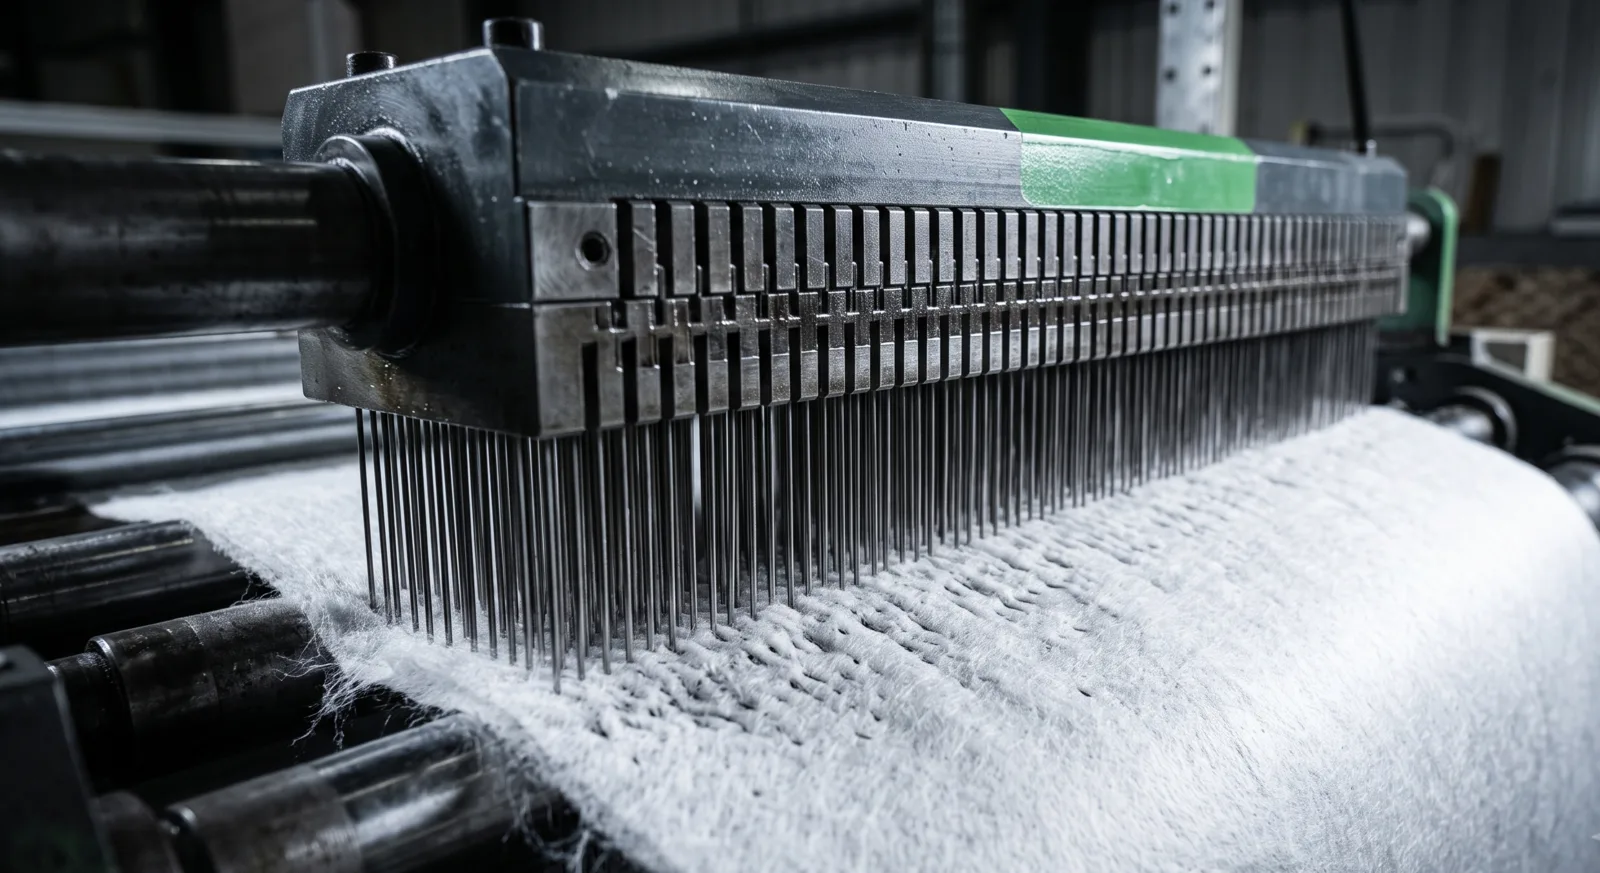
Fiber is bonded mechanically: tens of thousands of barbed needles punch through the fiber web, entangling the fibers so the layers lock together — no chemicals needed. This gives thick, strong, high-tensile fabric. It’s the most common technology for geotextile, carpet, industrial filter fabric and automotive materials. See the full breakdown in The needle-punch production process.
2. Spunbond
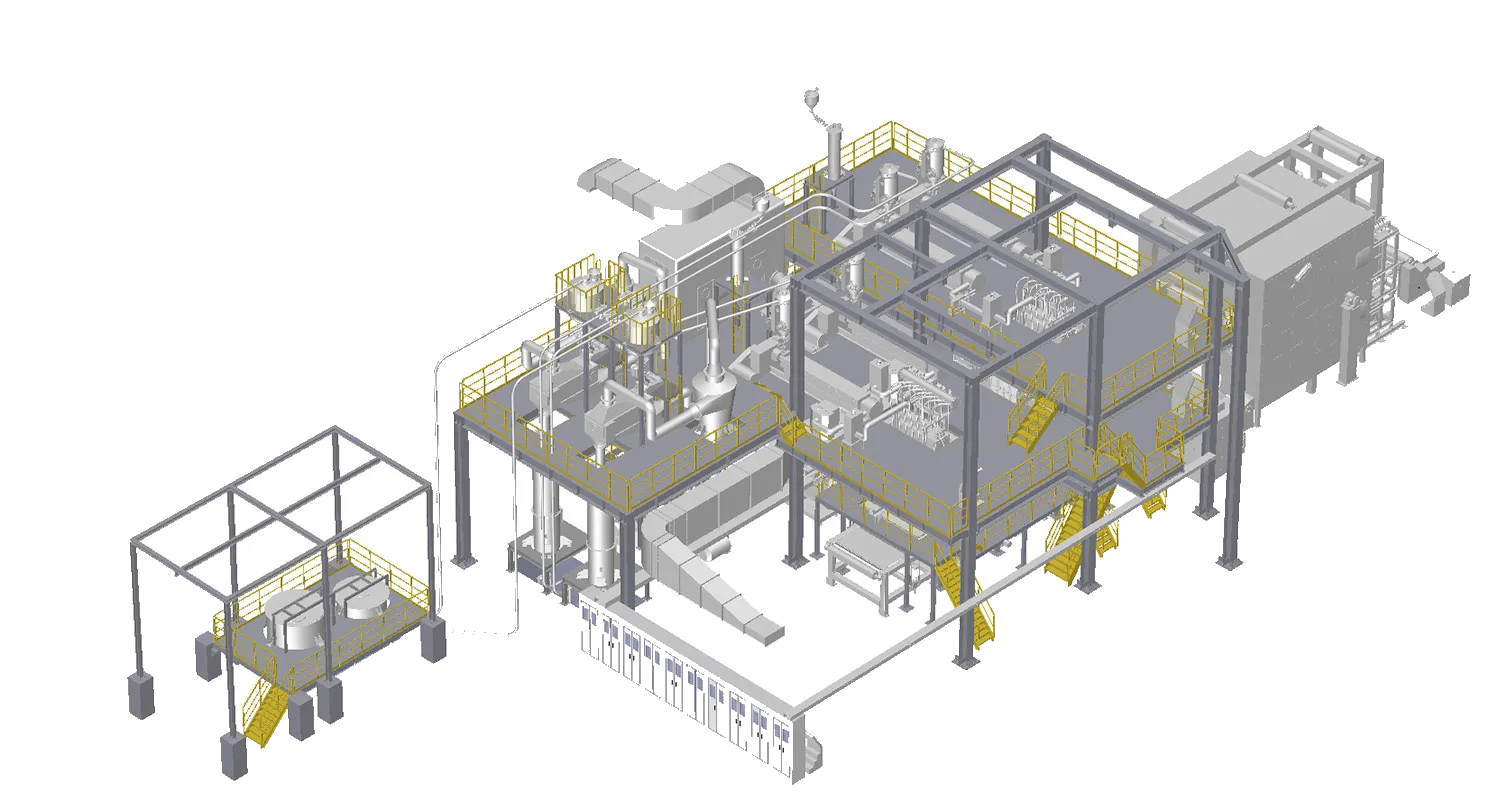
Polymer (usually PET) is melted, extruded into continuous filaments, laid directly into a web and thermally bonded on the same line — skipping the carding and cross-lapping steps used in needle punch. This gives thin, even fabric at very high output. See the full construction in The spunbond production line: construction and operating principle.
3. Meltblown
Molten polymer is blown by high-velocity air through a fine die, producing ultra-fine (micro) fibers. Meltblown fabric filters fine dust and bacteria well, and is commonly used as the filter layer in medical masks, layered with spunbond to form an SMS (spunbond–meltblown–spunbond) structure.
4. Spunlace (hydroentanglement)
The fiber web is bonded using high-pressure water jets instead of needles or heat, giving a soft fabric closer in feel to traditional woven cloth. Commonly used for wet wipes, medical fabric and single-use skin-contact products.
If you’re weighing the two most common technologies for industrial production, see the detailed comparison in Needle-punch vs spunbond: which technology should you choose?
How nonwoven fabric is actually produced (needle-punch line)
Unlike guides that describe nonwoven fabric only at a conceptual level, here’s the real machine chain a needle-punch line — the most common technology — runs in material-flow order:
- Bale opening & blending. Virgin or recycled PET/PP fiber is opened from compressed bales, cleaned of impurities and blended evenly before carding.
- Carding machine. Fiber is carded — parallelized and separated — into thin, even fiber webs. Carding quality depends directly on the card clothing / carding wire, a wear part that needs periodic replacement. The carding feeder at the input also determines how stable the GSM stays — see the feeder unit in a needle-punch line.
- Cross lapper. Layers the fiber web in a zigzag pattern to reach the target weight (GSM) and width, keeping the web even across the fabric — see the role of the cross lapper.
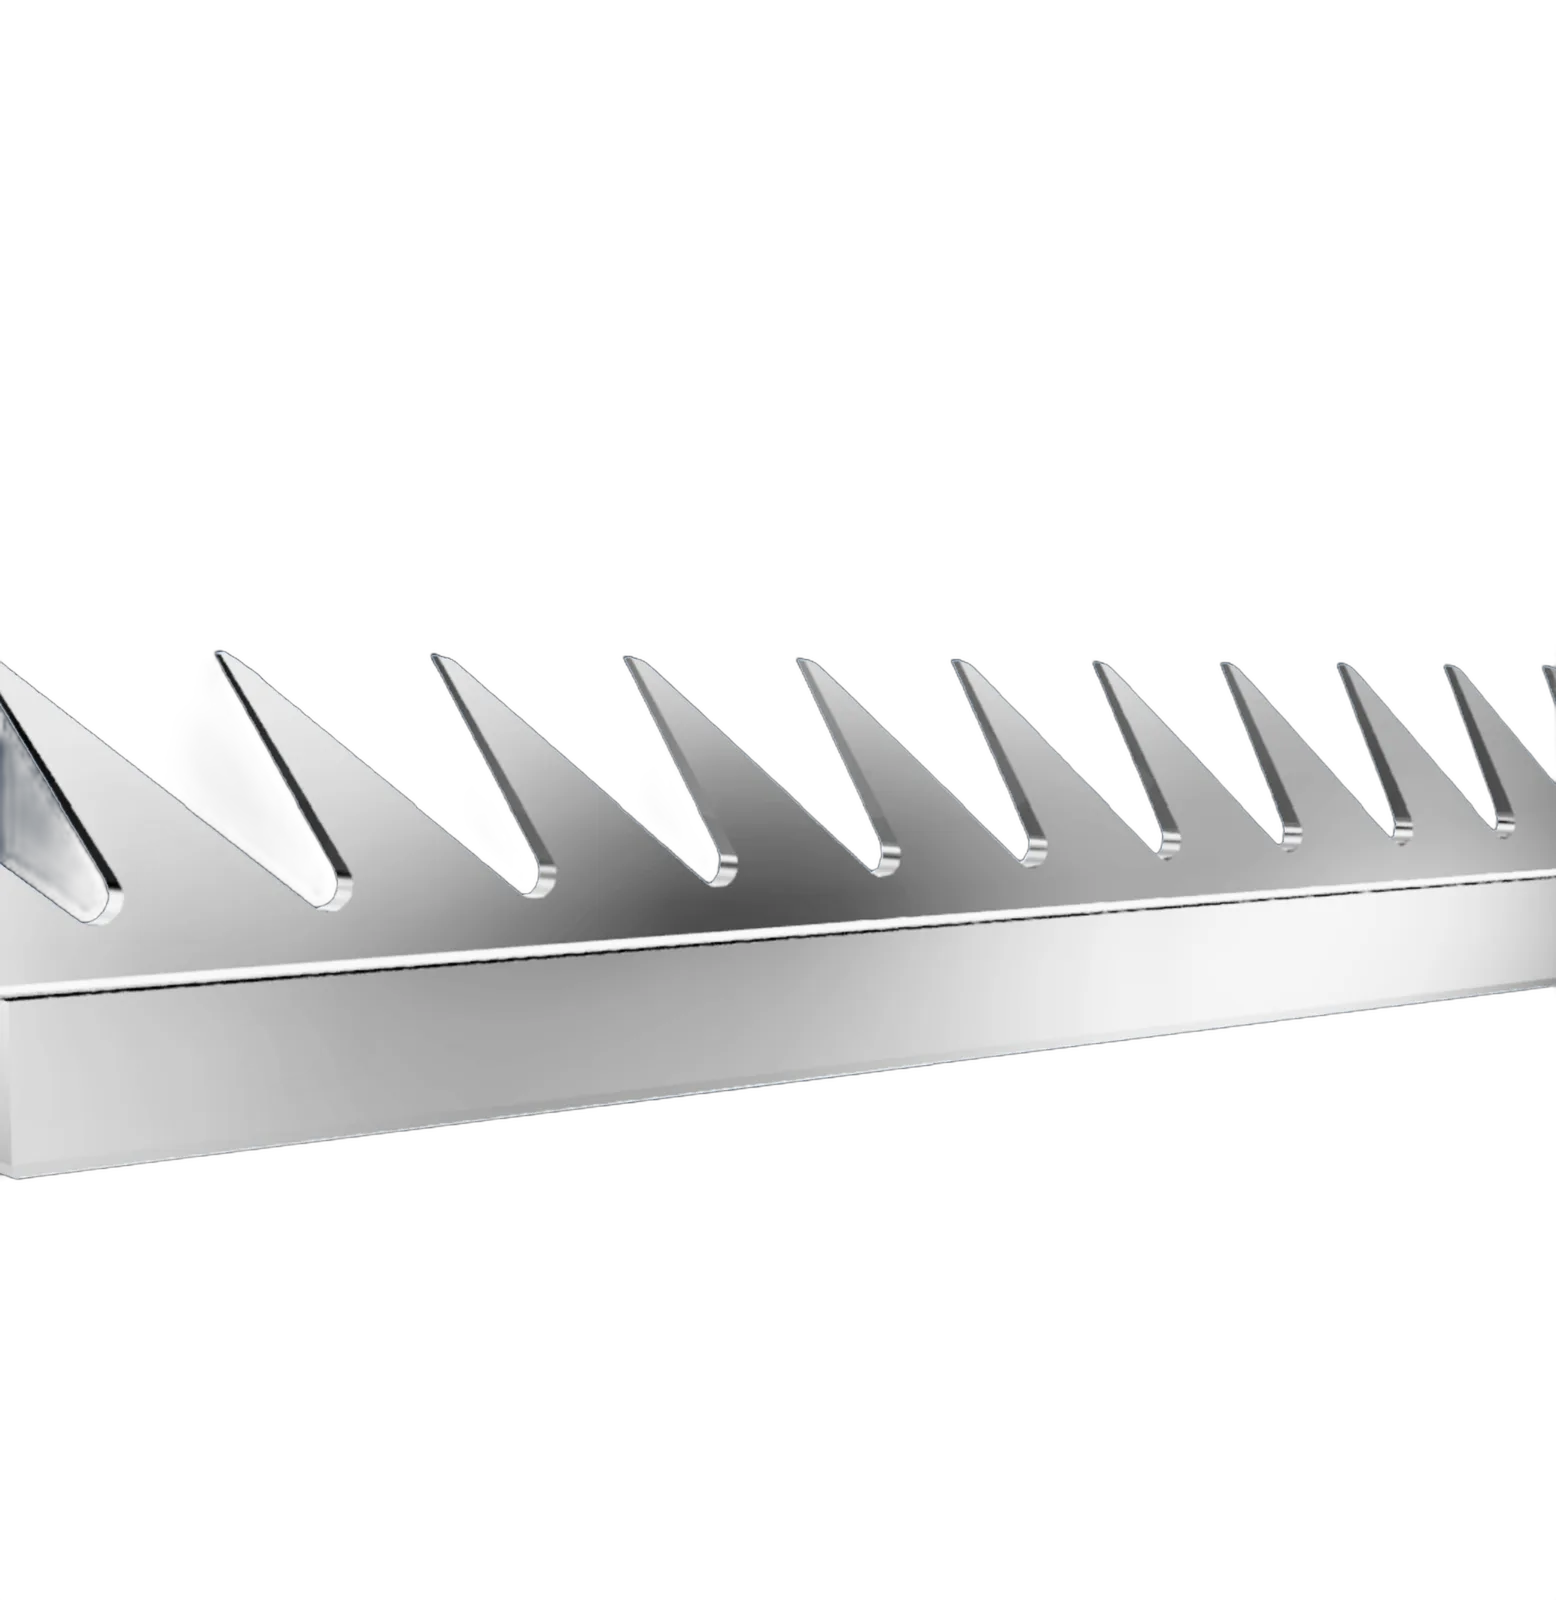
- Needle loom. Tens of thousands of barbed needles — mounted on needle boards — punch through the web, entangling fibers to mechanically bond the layers together. This stage creates the characteristic strength of needle-punch nonwoven.
- Calender / thermal finishing. May apply heat, pressure or coating to increase strength, smooth the surface, or finish the fabric for its target application.
- Winder. The stabilized fabric is wound into large rolls, ready for further processing or sale.
With spunbond, the carding – cross-lapping – needle-punch stages are replaced by continuous filament spinning and thermal bonding on the same line, giving higher output but thinner fabric.
If you’re planning an investment, What machines do you need to open a nonwoven workshop? covers all 6 machine groups in a complete line, and What determines the cost of investing in a nonwoven line? explains the cost factors.
Applications of nonwoven fabric
- Geotextile. Thick, strong, water-permeable needle-punch nonwoven separates material layers, reinforces soil, and filters and drains water in roads, dikes and landfills. See Which line makes geotextile fabric?
- Automotive. Nonwoven fabric forms interior lining, floor mats and acoustic/thermal insulation inside vehicles — usually requiring the high mechanical strength that needle punch delivers.
- Medical. Masks, protective gowns and surgical drapes — mostly made with spunbond combined with meltblown (SMS structure) or spunlace for skin-contact products.
- Industrial filtration. Dust, air and oil filters need a thick, porous fiber structure, typically made by needle punch or meltblown depending on the particle size to be filtered.
- Home furnishing. Upholstery, carpet and decorative lining fabric make use of the thickness and hand-feel of needle-punch nonwoven or the softness of spunlace.
Quick comparison with traditional woven fabric
| Criteria | Nonwoven fabric | Traditional woven fabric |
|---|---|---|
| How structure forms | Direct fiber bonding (mechanical/thermal/chemical) | Yarn spun then interlaced in 2+ directions (weaving/knitting) |
| Number of stages | Fewer — skips spinning and weaving | More — spinning, sizing, weaving, finishing |
| Production speed & cost | Faster, lower cost per meter | Slower, higher cost |
| Directional strength | Often skewed toward machine direction (MD) unless treated | More balanced across both weave directions |
| Thickness/GSM flexibility | Very flexible via layering and needling density | Limited by weave pattern and yarn density |
| Typical applications | Geotextile, filtration, single-use medical, automotive | Apparel, premium home textiles, long-life fabric |
Conclusion
Nonwoven fabric is a material made by bonding fiber directly — without weaving or knitting — with four main technologies: needle punch, spunbond, meltblown and spunlace, each suited to a different group of applications. Understanding the right technology and production process helps a business choose the right line for the product it wants to make, rather than looking only at the finished fabric.
Vina Nonwoven is the Vietnam distributor of needle-punch lines (Zhentai) and PET Spunbond lines (Huayang) — the two most common nonwoven production technologies — with spare parts, installation and maintenance handled locally. Contact us by hotline or Zalo for advice on the technology that fits your product and a quote.